Handling Procedures and Preventive Measures for Soft Electrode Breakage in Production
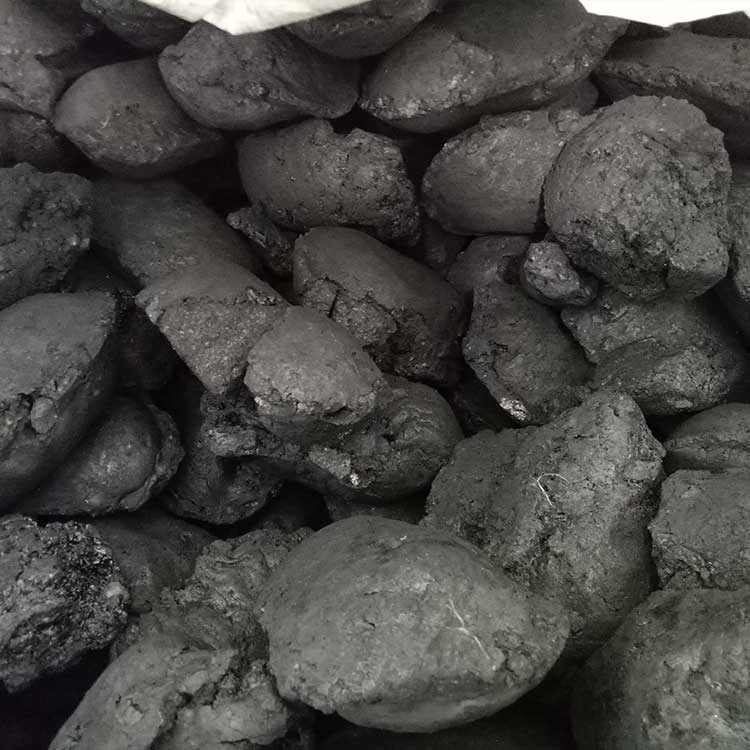
1. Once a soft electrode break is detected, power should be immediately cut off. Operators should avoid gathering too closely; the main operator should handle the situation. Quickly lower the electrode into the furnace to prevent electrode paste from leaking out. Loosen the electrode promptly so that it connects with the broken end. Remove and clear away the electrode paste around the broken area. Then restore power and carry out low-load roasting. The affected electrode must not be raised during this process. Load can be gradually increased according to the electrode's roasting condition, and full roasting typically takes about 6 to 8 hours.
2. If the broken end cannot be reconnected and the electrode paste has dried up completely, making flow impossible, release some of the electrode—amount depending on electrode size—and proceed with low-load roasting using the same method as above.
3. If the electrode tip cannot be reconnected and the paste is very runny, possibly causing large-scale leakage or nearly emptying the paste near the electrode, weld an additional section with a base similar to the electrode tip used at new furnace startup. Add fresh electrode paste and continue roasting as before, but pay special attention to air supply volume and cooling water flow to the conductive jaw plates.
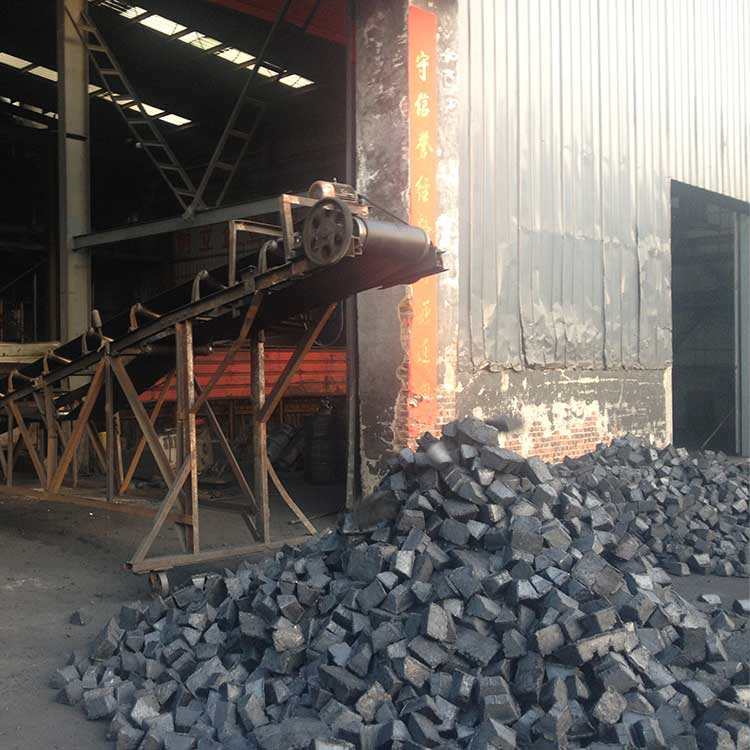
1. Properly control the electrode air supply and cooling water flow to the conductive jaw plates. This requires operators to conduct thorough inspections regularly, adjusting airflow and water flow promptly to ensure normal electrode roasting.
2. Exercise extreme caution when pressing down electrodes. When increasing load, act decisively yet carefully, closely observing any changes in the electrode. If electrode deterioration is observed, reduce the load immediately and, if necessary, cut off power for handling.
3. Regularly inspect electrode paste quality and never use substandard paste.
4. Strictly check the quality of electrode shells and welding work, ensuring compliance with technical specifications and quality standards.
5. Strictly follow electrode management procedures: lower electrodes according to schedule, carefully control time intervals between lowering operations, refill electrode paste on time, and maintain specified electrode height and working length.
 Phone:+86 19937179450
 Whatsapp:+86 19937179450
 Email:
 Add:Zhengdong New District,Zhengzhou City,China.